Mill Turning Services

We produce complex rotational components that combine precision diameters with milled flats, ports, cross-holes, bolt patterns and angled features. MAZAK Y-axis live tooling, TSUGAMI dual-spindle back-working and DESHAN multi-axis capability reduce machine transfers and protect feature-to-feature relationships, supported by DFM and drawing-defined inspection for aerospace, semiconductor, robotics and medical applications.

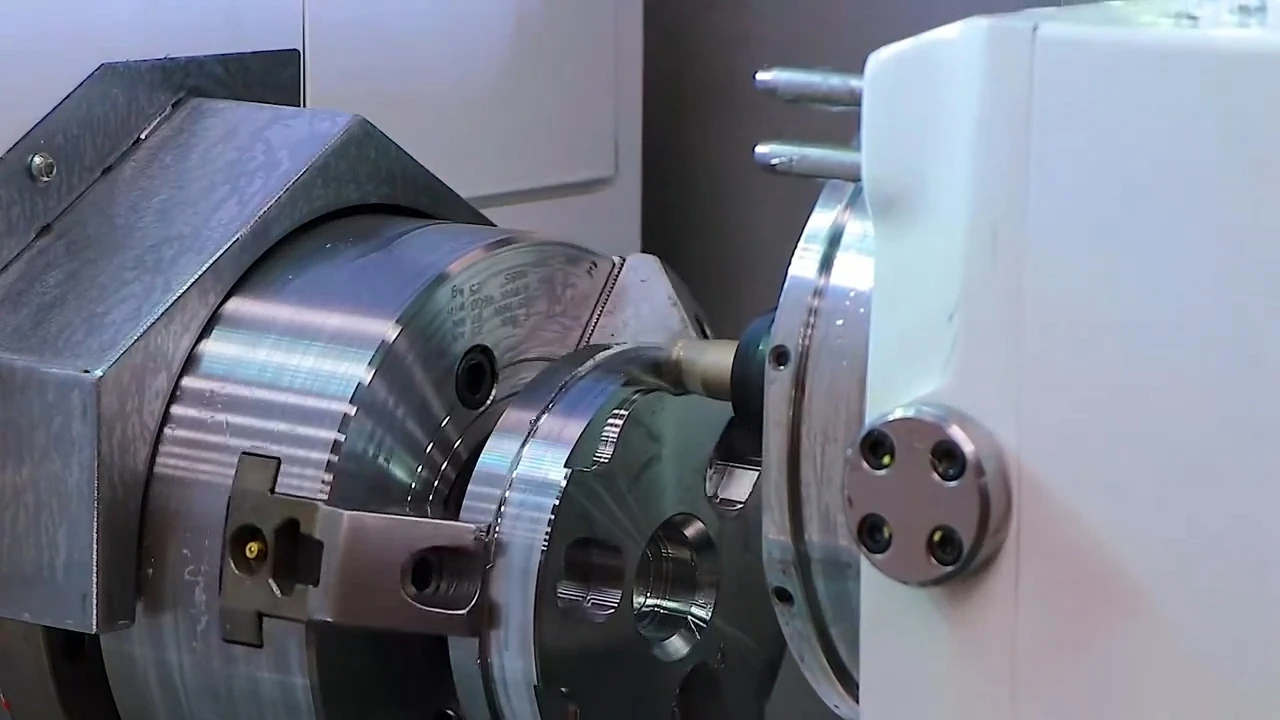
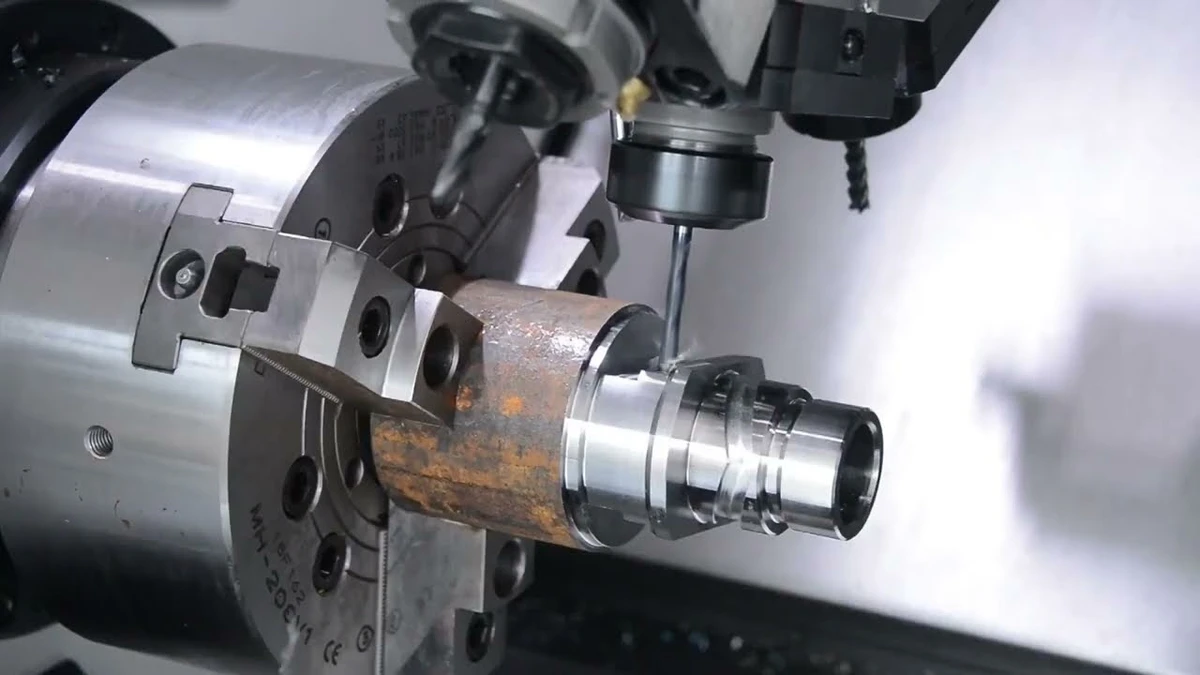
Mill-turn machining of a metal flange held in a chuck

Mill-Turn Machining Capacities

Our mill-turn machining services combine turning spindles, live milling, Y-axis travel, and sub-spindle back-working in a single machine — producing complex parts with turned profiles, milled flats, cross-holes, and off-axis features complete in one clamping. The coordinated route protects feature-to-feature relationships. Standard tolerances are ±0.02 mm, with ±0.005 mm reviewed for critical features; the agreed drawing, setup and inspection plan determine the final capability.

We support prototype and repeat-production orders for manifolds, fittings and other rotational components. Programs and first parts are verified before repeat production; inspection coverage and records follow the agreed order requirements. Complete RFQs receive an initial engineering response within one working day; the quotation follows confirmation of the manufacturing scope.

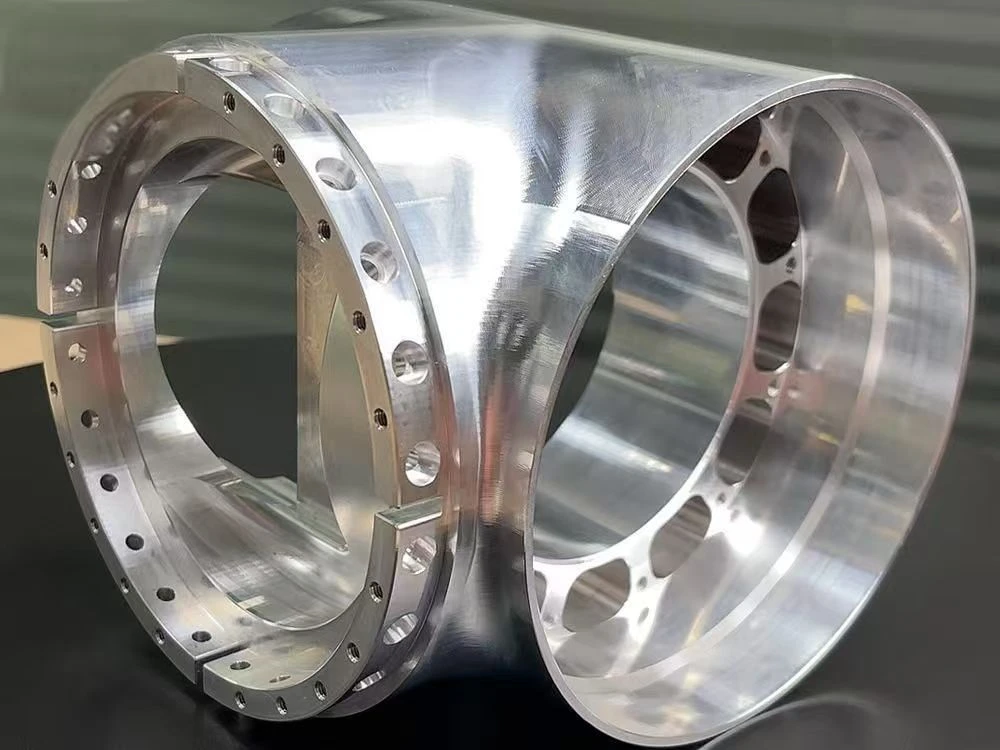
Machined metal housing with large intersecting bores, flanges and drilled mounting holes

The Mill-Turn Machines We Run

Our mill-turn resources combine Y-axis live tooling, dual-spindle back-working and multi-axis access to complete turning, milling, drilling, tapping, angled holes and rear-side features with fewer setups. Machine selection follows the diameter and length envelope, bar or chucking route, material behavior, feature relationships and inspection access.

MAZAK

A rigid turning platform with Y-axis live tooling for combining precision diameters, bores and threads with milling, drilling and tapping in one coordinated setup.

  • Fanuc 0i-TF Plus / MAZATROL SmoothC
  • 12-station turret
  • 6,000 rpm
  • Turning Ø350 × 500 mm

TSUGAMI

Dual-spindle machining transfers the component for rear-side facing, boring, threading and related operations without moving it to a separate machine and fixture.

  • Fanuc 0i-TF
  • 12-station turret
  • 4,500 rpm
  • Turning Ø280 × 240 mm

DESHAN

A multi-axis route for angled holes, off-axis features and complex profiles on turned components where access and feature relationships justify the additional movement.
  • Syntec 22TB control
  • 15-station turret
  • 4,500 rpm
  • Travel X600 × Y90 × Z500 mm

Capacity And Tolerances

The values below describe our confirmed general mill-turn envelope. Dimensional values are specified in millimeters; inch equivalents are rounded. Final capability depends on material, stock form, wall thickness, unsupported length, tool reach, feature relationships and measurement access. The central advantage is not only an individual diameter tolerance, but the ability to control turned and milled features from a common setup when runout, true position or perpendicularity is functionally critical.

CapabilitySpecification
Max turning diameterØ340 mm
Max turning length553 mm
Maximum bar capacityØ52 mm
Y-axis travel100 mm
Standard tolerance±0.02 mm (±0.0008 in)
Precision tolerance±0.005 mm (±0.0002 in) on critical features, subject to drawing review
Concentricity0.01 mm with single-setup machining
Surface finishRa 0.8 µm as machined; Ra 0.4 µm with precision finishing
Main spindle speedUp to 6,000 rpm
Live tool speedUp to 4,500 rpm
Live tooling capacityDrilling Ø20 mm / milling Ø20 mm / tapping M20 × 2.5
Batch size1 prototype to 10,000+ production parts
Typical lead time5–15 working days

How Our Mill-Turn Service Process Works

The manufacturing sequence covers drawing and technical requirements review, process planning, incoming material inspection, first article inspection, production machining, surface treatment and final inspection. Machining instructions and inspection records are tied to the approved drawing revision and production batch.

Materials We Machine

Material behavior influences tool selection, heat control, chip evacuation, workholding and the balance between turning and milling operations. We review bar, prepared blanks, forgings or castings against machining allowance, stock condition, hardness and traceability requirements; material certificates, including EN 10204 3.1 where specified, can accompany the order.

ImageMaterial FamilyRegular GradesPerformance AdvantagesTypical Applications
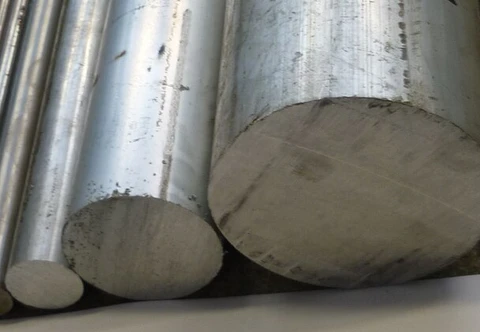
Short cylindrical metal blank with a bright sawn end faceAluminum
  • 6061-T6
  • 7075-T6
  • 2024-T3
  • 5083
  • cast aluminum
Low density, good machinability and high thermal conductivity; selected grades provide a strong strength-to-weight ratio.Robotics frames, semiconductor chambers, aerospace brackets
Round metal stock showing solid circular cut endsStainless Steel
  • 303
  • 304
  • 316L
  • 17-4PH
  • 15-5PH
  • 440C
Corrosion resistance, mechanical strength and clean-service compatibility; precipitation-hardening grades add higher strength.Vacuum and semiconductor parts, robotics fittings
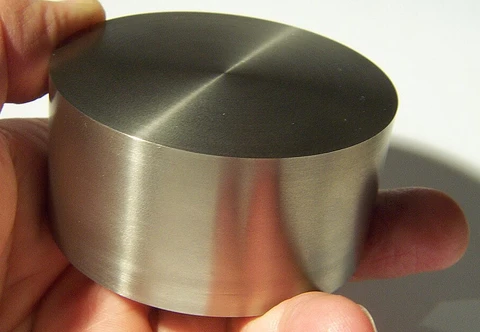
A short titanium cylinder held in a hand, with a flat circular end and straight sidesTitanium
  • Ti-6Al-4V (Grade 5)
  • Ti-6Al-4V ELI
High strength at low weight, excellent corrosion resistance and dependable performance at elevated temperatures.Aerospace structural and engine components
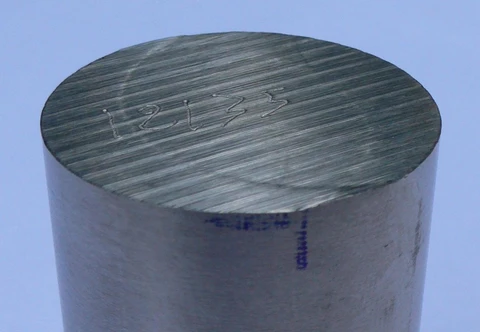
Cylindrical Inconel stock with a visible cut end faceSuperalloys
  • Inconel 718
  • Inconel 625
  • Monel 400
Retains strength under heat and resists oxidation, corrosion and creep in demanding operating environments.Aerospace turbine and high-temperature parts
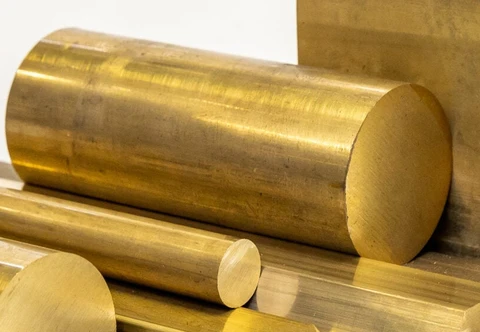
A solid brass cylinder with a circular cut face and visible machining linesCopper & Alloys
  • C110
  • C17200 beryllium copper
  • C260 brass
High electrical and thermal conductivity; selected alloys add strength, fatigue resistance and wear performance.Semiconductor electrodes, ESD-conscious robotics parts
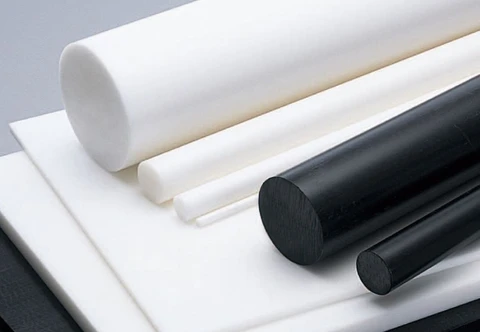
White and black polymer round stock with solid circular endsEngineering Plastics
  • PEEK
  • PEI (Ultem)
  • POM
  • PVDF
Low mass, chemical resistance and electrical insulation, with selected grades suited to heat, low friction or dimensional stability.Wafer handling, lightweight robotic components
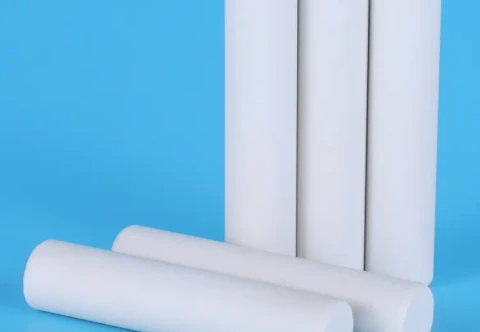
Solid white ceramic cylindrical blanks on a blue surfaceCeramics
  • Alumina 99.5%
  • Zirconia
  • SiC
  • AlN
High hardness, wear and heat resistance, electrical insulation and stable performance in clean or corrosive environments.Semiconductor insulators, wafer chucks and wear components
Round metal stock showing solid circular cut endsTool & Alloy Steel
  • 12L14
  • 1045
  • 4140PH
  • H13
  • D2
  • 8620
High strength, hardness and fatigue resistance, with heat-treatment options for wear surfaces and load-bearing features.Robotics reducers, shafts, couplings and gears

Surface Finishes

Finishing is planned with coating allowance, masking, thread protection, sealing surfaces and post-process verification in mind. In-house and qualified partner processes are managed under one purchase order, with critical features rechecked after finishing when required by the drawing or control plan.

As-MachinedRa Per Machining Route And Drawing

A finish left directly by the cutting process, with controlled tool marks and no additional surface treatment. The process capacity table and drawing define the required roughness.
Typical Applications: Robotics journals and bearing seats

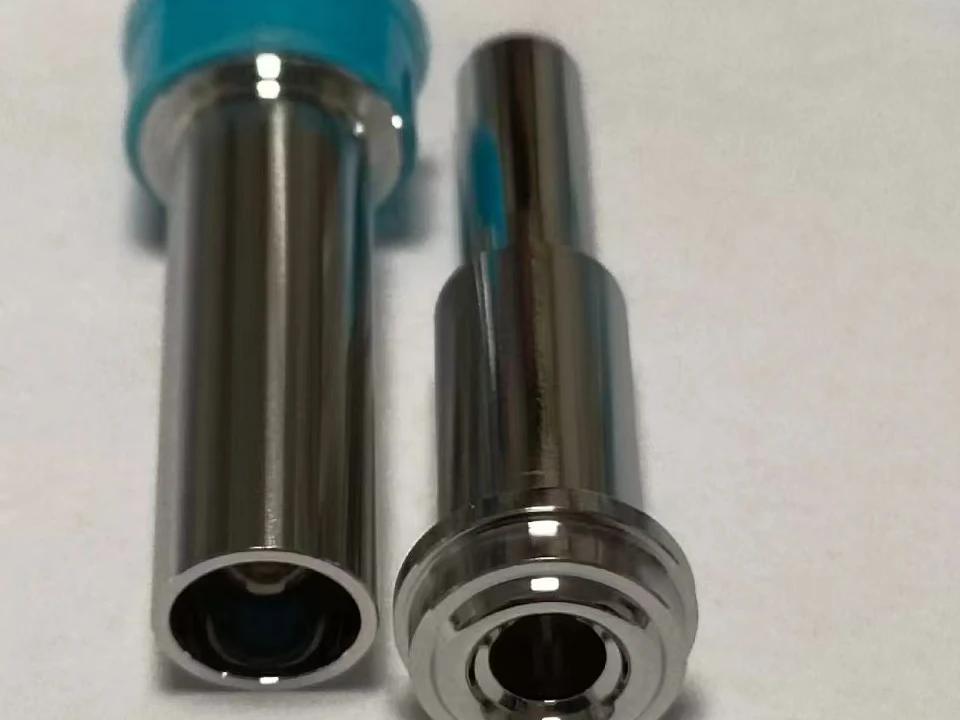
PolishingRa 0.2 µm

A mechanical finishing process that smooths the surface to reduce roughness and improve sealing, cleanability or appearance.

Typical Applications: Semiconductor sealing faces and vacuum bores

Two polished metal components with reflective cylindrical surfaces and hollow bores
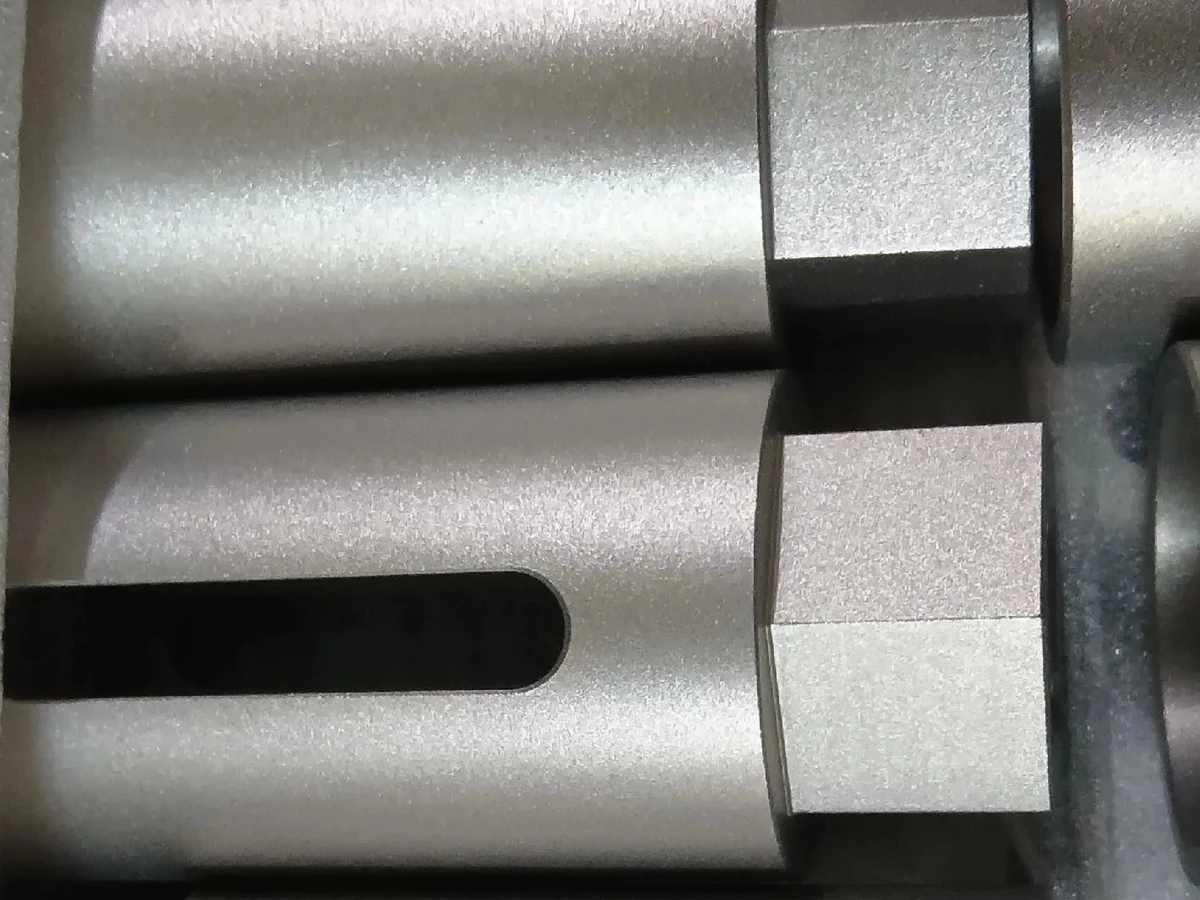
Bead BlastingUniform matte texture

A surface treatment that creates a uniform matte texture by blasting fine abrasive media onto the part surface.

Typical Applications: Aerospace and robotics surfaces

Matte-textured cylindrical metal components with flats and a longitudinal slot
Anodizing (Type II)Natural or custom color; thickness, sealing and masking per drawing

Type II anodizing builds a protective oxide layer on aluminum for corrosion protection and appearance. Clear natural and dyed finishes are color options within the same process. A custom color reference and acceptance sample can be specified.

Typical Applications: Aluminum housings, robotics arms, brackets and visible components

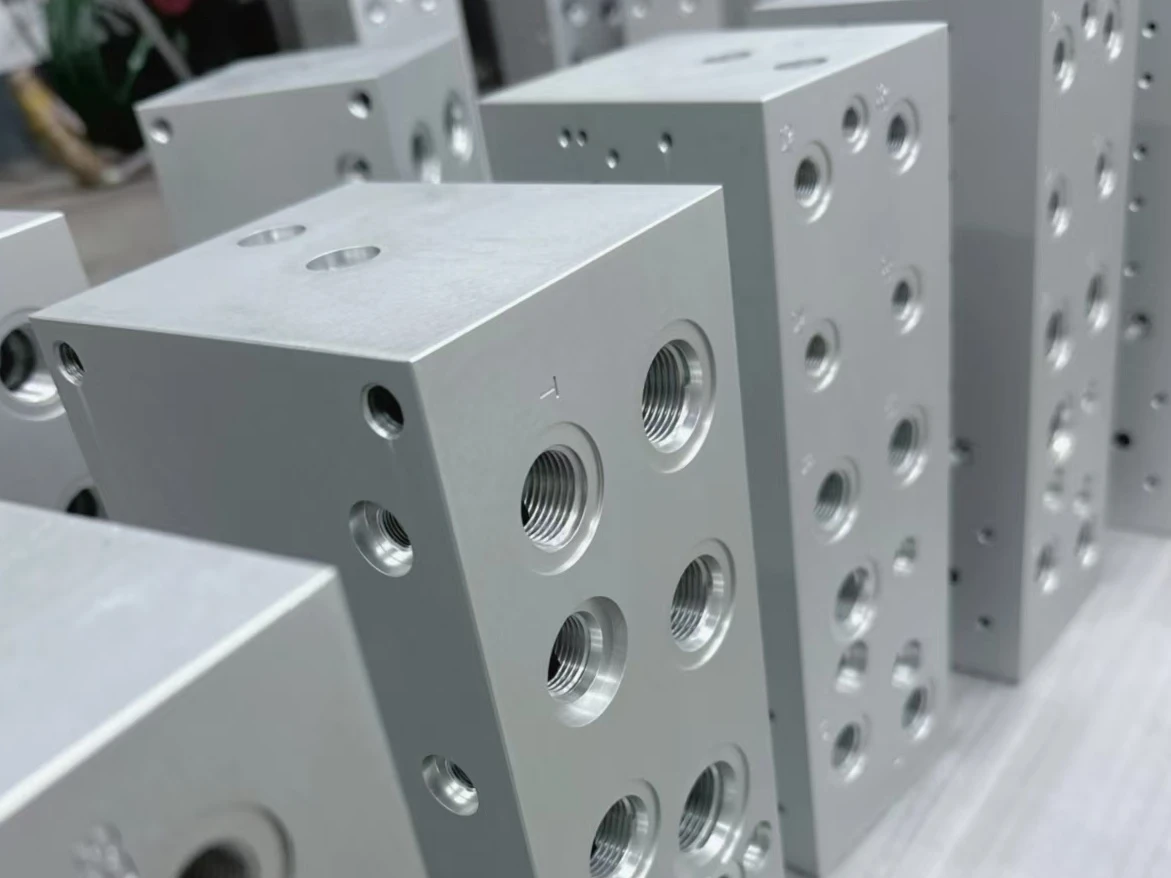
Natural-colored anodized metal blocks with threaded bores and side holes
Hard Anodizing (Type III)Type III hardcoat; thickness, sealing and masking per drawing

Hard anodizing is selected for wear-resistant aluminum surfaces. Coating allowance and masking are planned around critical fits; any hardcoat color requirement is reviewed with the specified alloy and thickness.

Typical Applications: Sliding guides, bushings and wear-contact aluminum components

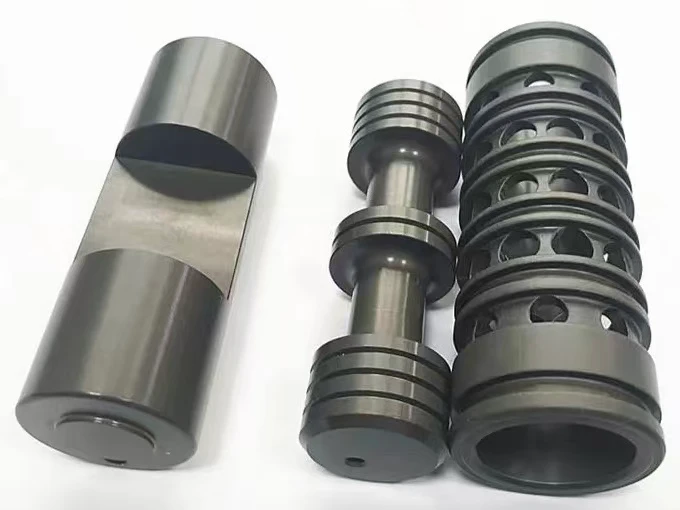
Dark hard-anodized cylindrical parts with grooves, shoulders and machined flats
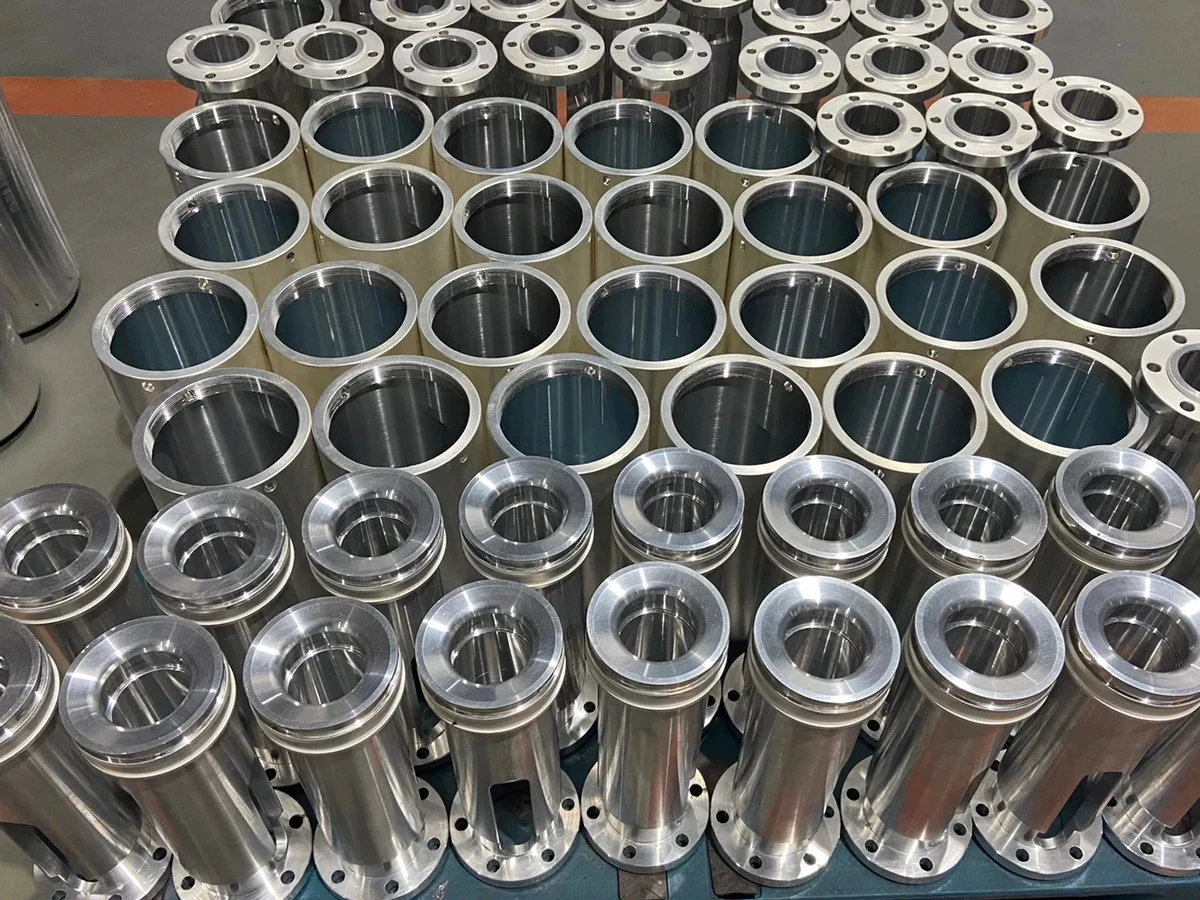
PassivationAMS 2700 / ASTM A967

A chemical treatment for stainless steel that removes free iron from the surface and supports its natural corrosion resistance.

Typical Applications: 316L semiconductor and vacuum parts

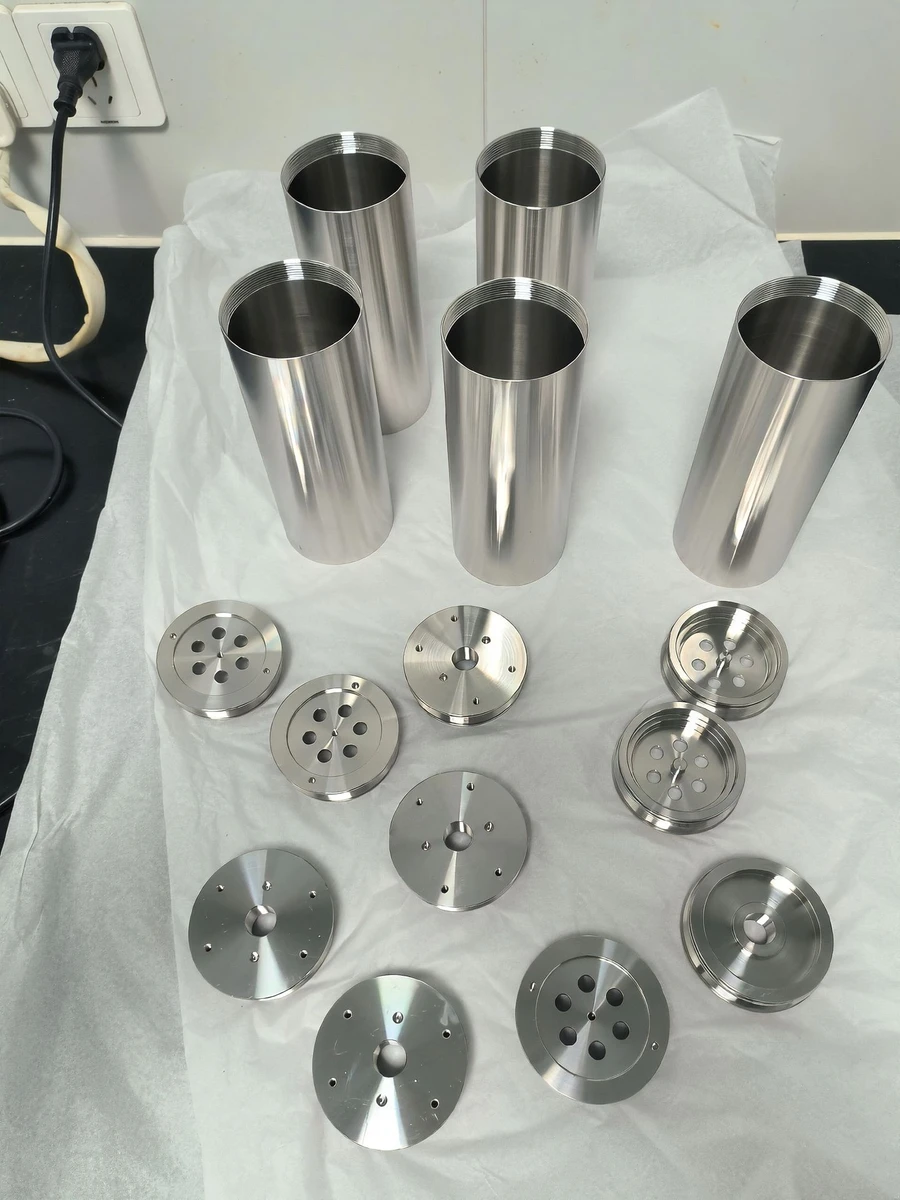
Stainless cylindrical housings and circular end plates arranged on a white sheet
Electroless Nickel Plating5–50 µm, uniform on bores

A chemically deposited nickel coating that provides consistent thickness on complex geometry and improves corrosion and wear resistance.

Typical Applications: Semiconductor chambers and robotic leadscrews

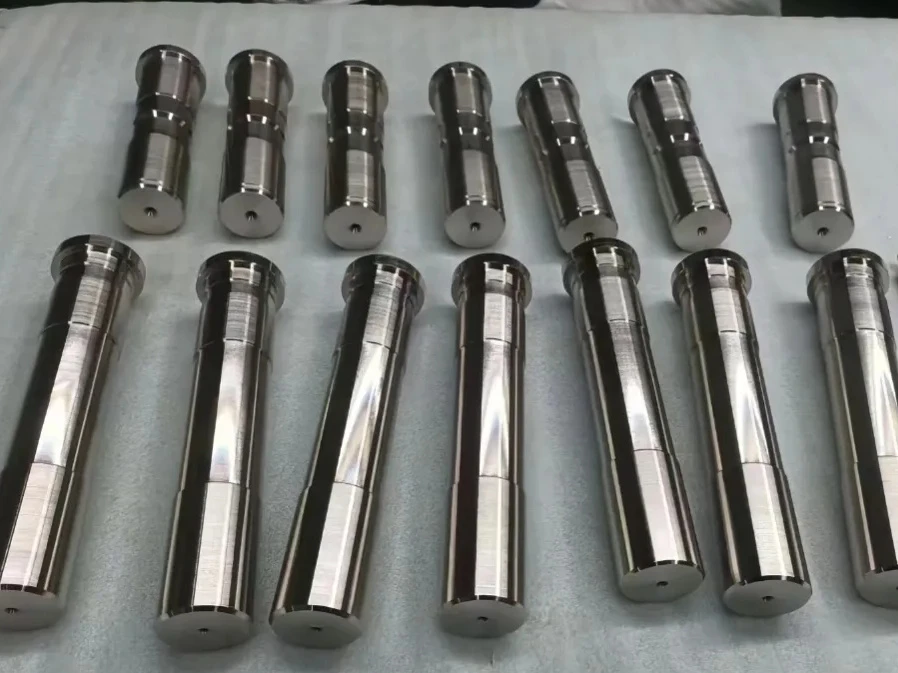
Nickel-finished metal shafts with stepped diameters arranged on a white sheet
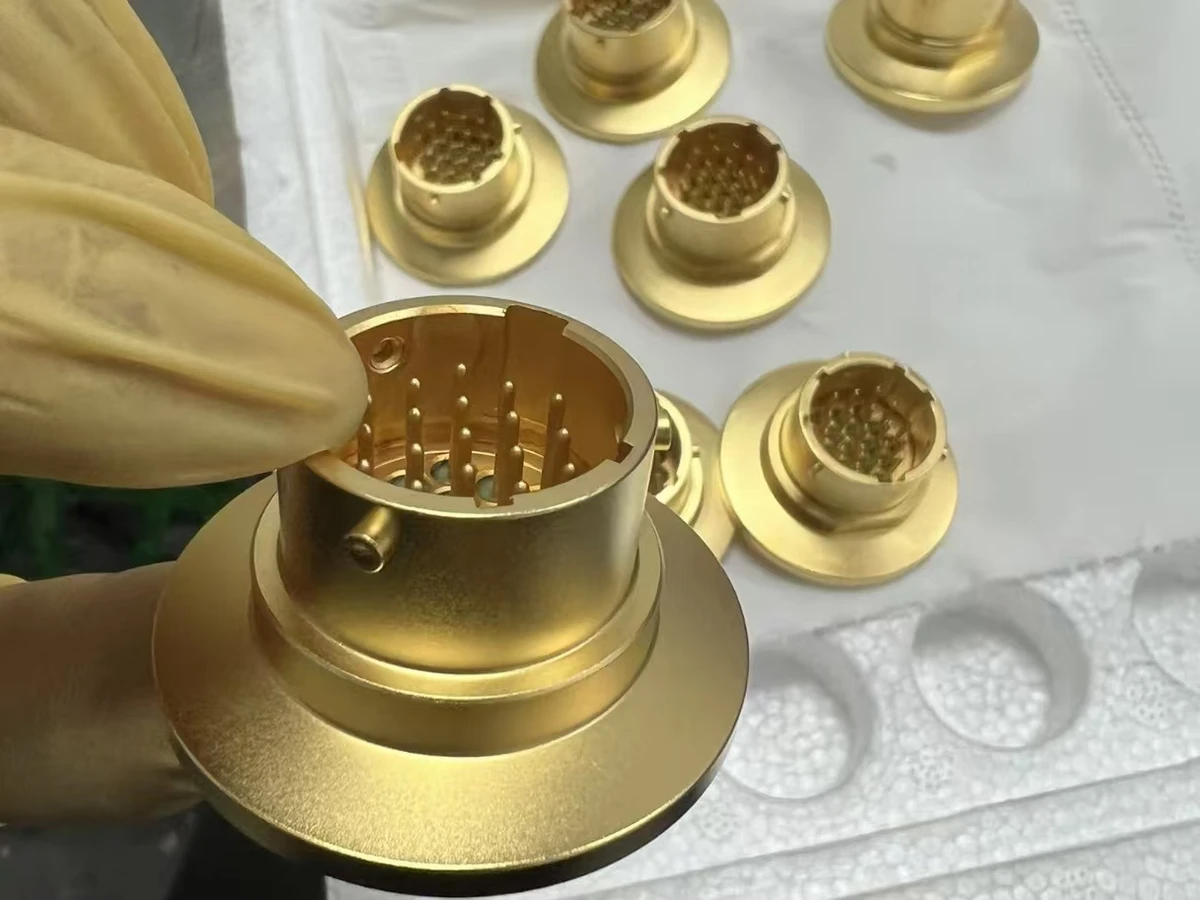
Gold PlatingPer semiconductor specification

A corrosion-resistant precious-metal coating that provides stable electrical contact performance and low contact resistance.

Typical Applications: Precision contacts and semiconductor electrodes

Gold-colored connector housings with flanges and contact pins
Silver PlatingPer semiconductor specification

A highly conductive metallic coating used to improve electrical and thermal transfer on functional component surfaces.

Typical Applications: High-current contacts and conductive components

Silver-finished cylindrical components with bores and mounting flanges arranged in rows
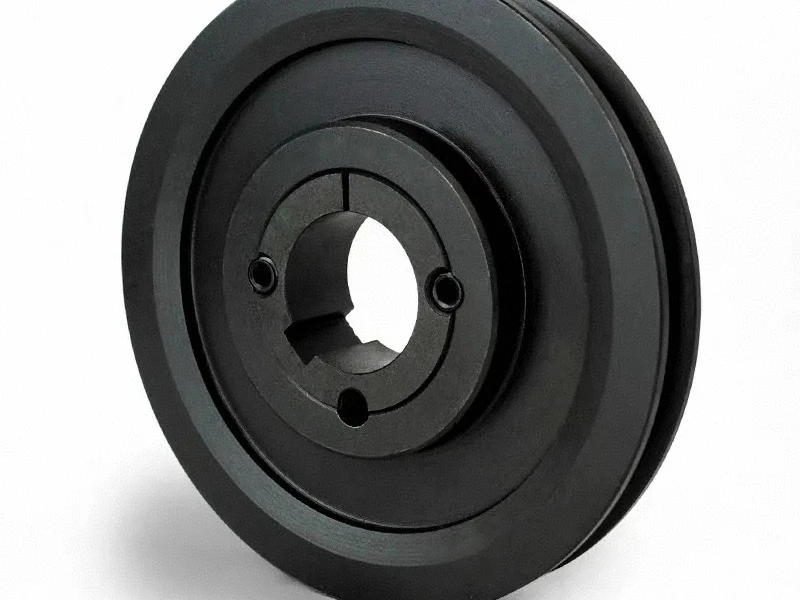
Black OxideDrawing-specified military standard

A thin conversion finish for ferrous metals that reduces glare and adds mild corrosion protection with the specified seal or oil.

Typical Applications: Steel fasteners, tooling and fixtures

Black-finished circular metal component with a keyed bore and concentric steps
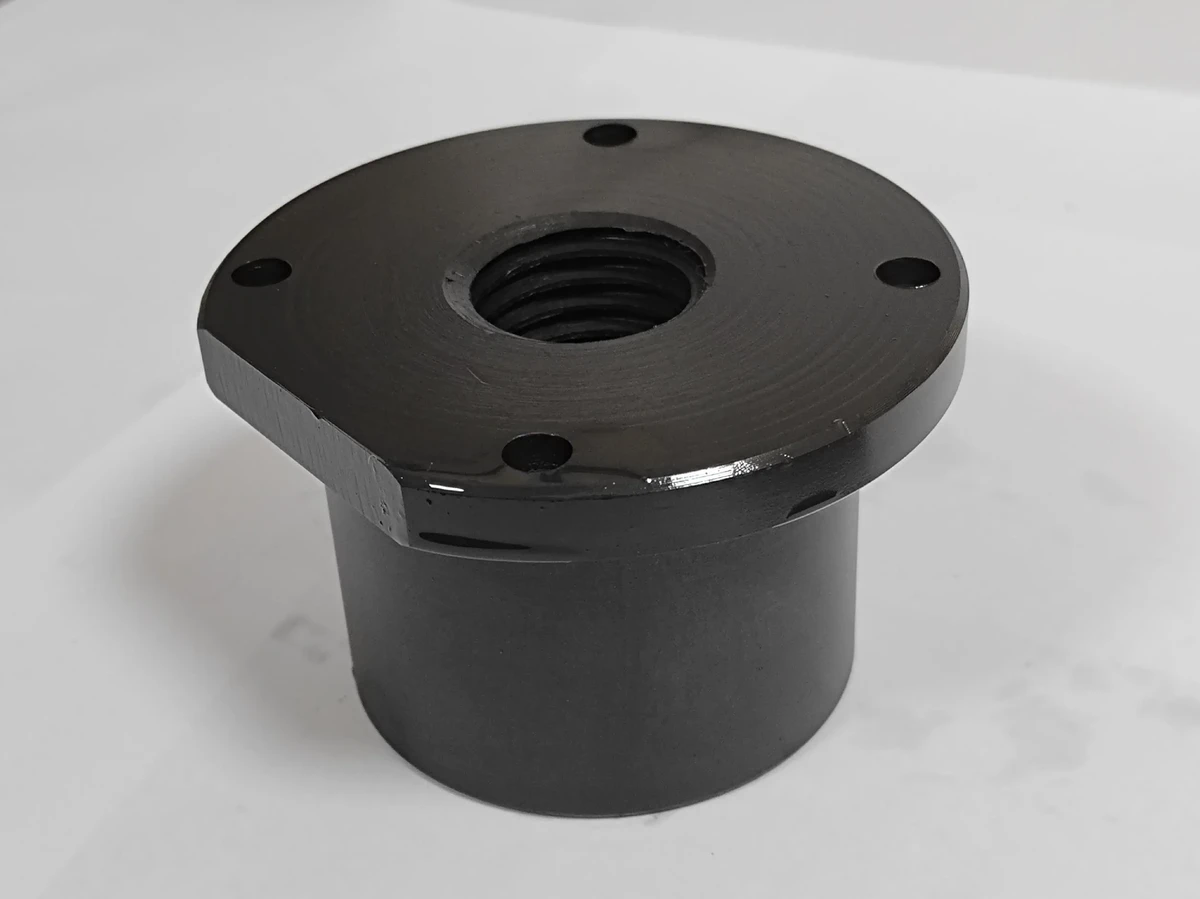
Phosphate CoatingDrawing-specified military standard

A crystalline conversion coating for steel that improves lubricant or paint adhesion and supports wear-in and corrosion protection.

Typical Applications: Aerospace fasteners and wear components

Dark phosphate-finished cylindrical component with an internally threaded flange
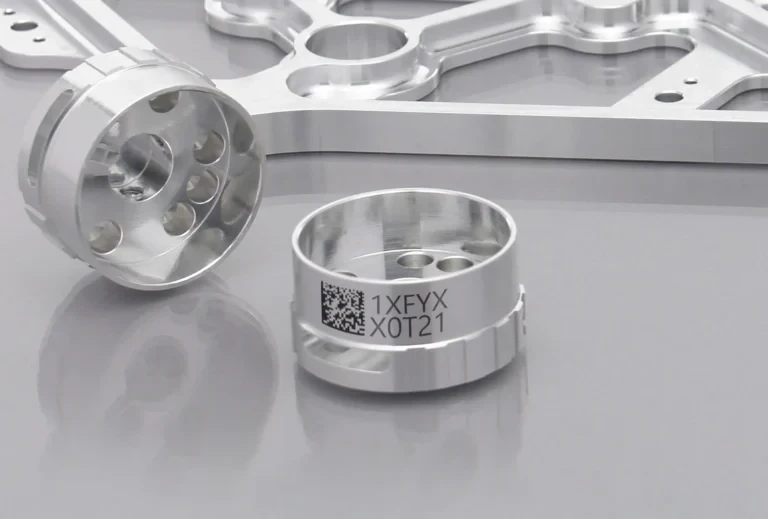
Laser EngravingDeep or surface marking

A permanent marking process for part numbers, lot codes and traceability without adding a separate label.

Typical Applications: Traceability and part numbers

Machined metal ring with a two-dimensional code and alphanumeric laser marks on its outer surface
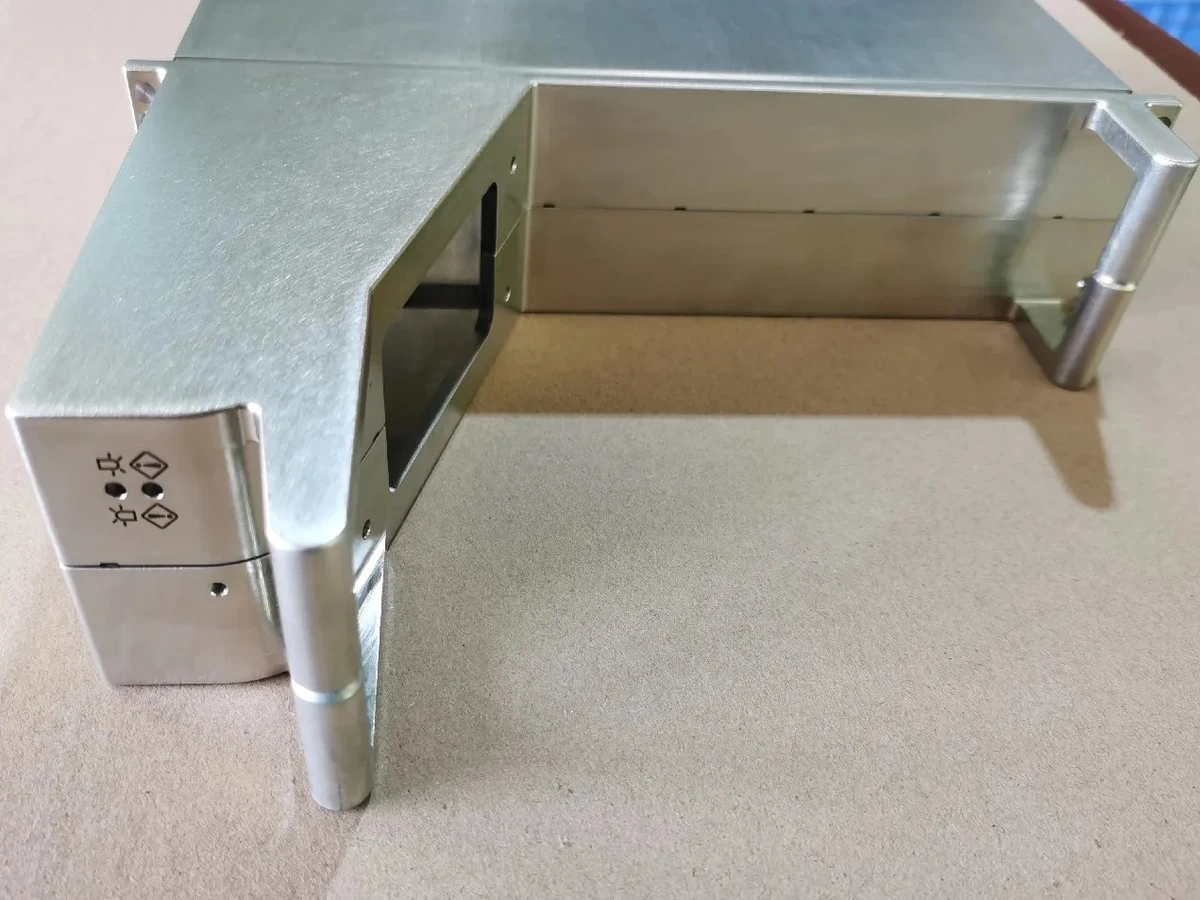
Zinc PlatingDrawing-specified thickness and chromate

An electroplated zinc layer provides sacrificial corrosion protection for carbon and alloy steel components with controlled coating thickness.

Typical Applications: Steel fittings, couplings and industrial hardware

Zinc-finished metal enclosure with machined openings and corner posts
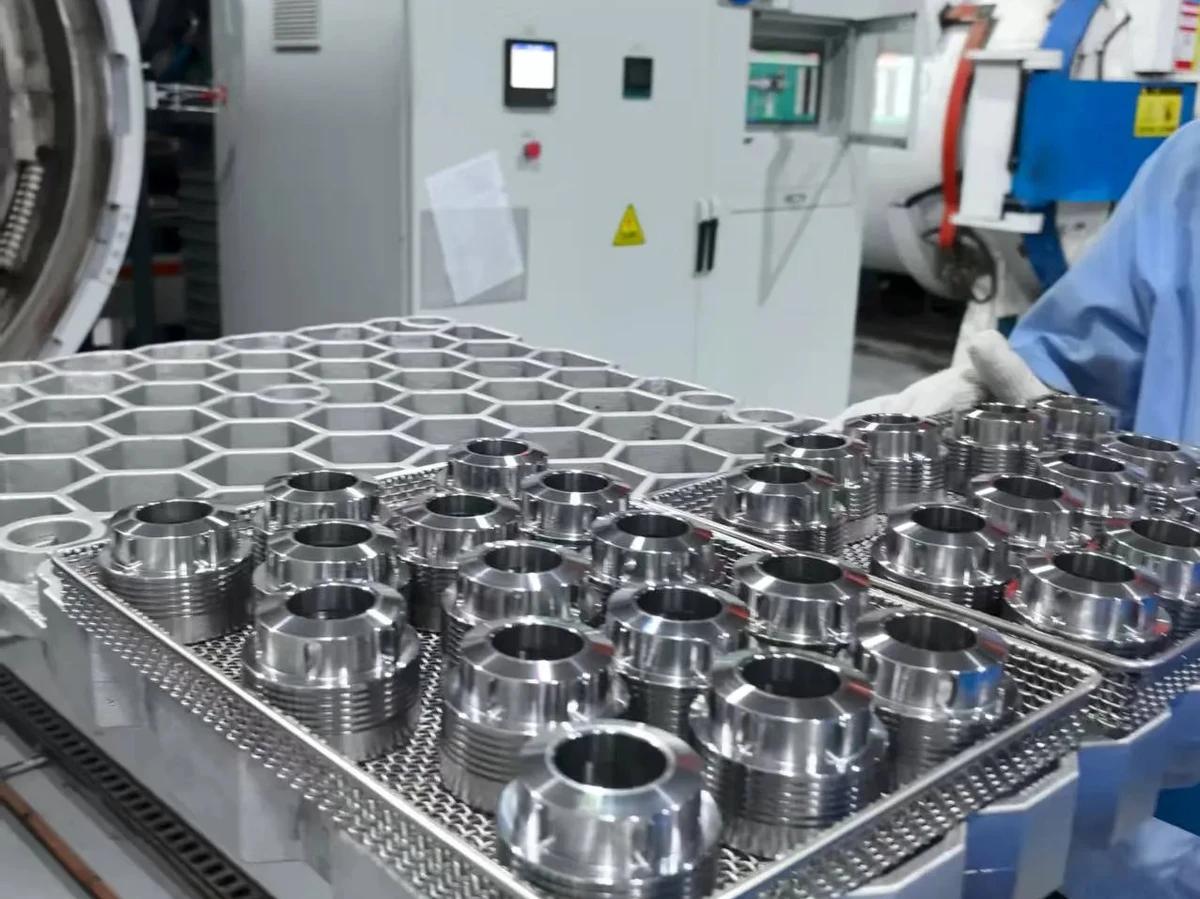
Heat TreatmentHardness per drawing

Through-hardening, case hardening or precipitation hardening is coordinated with material grade, distortion allowance and final verification.

Typical Applications: Shafts, couplings, gears and wear features

Metal components on processing trays beside heat-treatment equipment
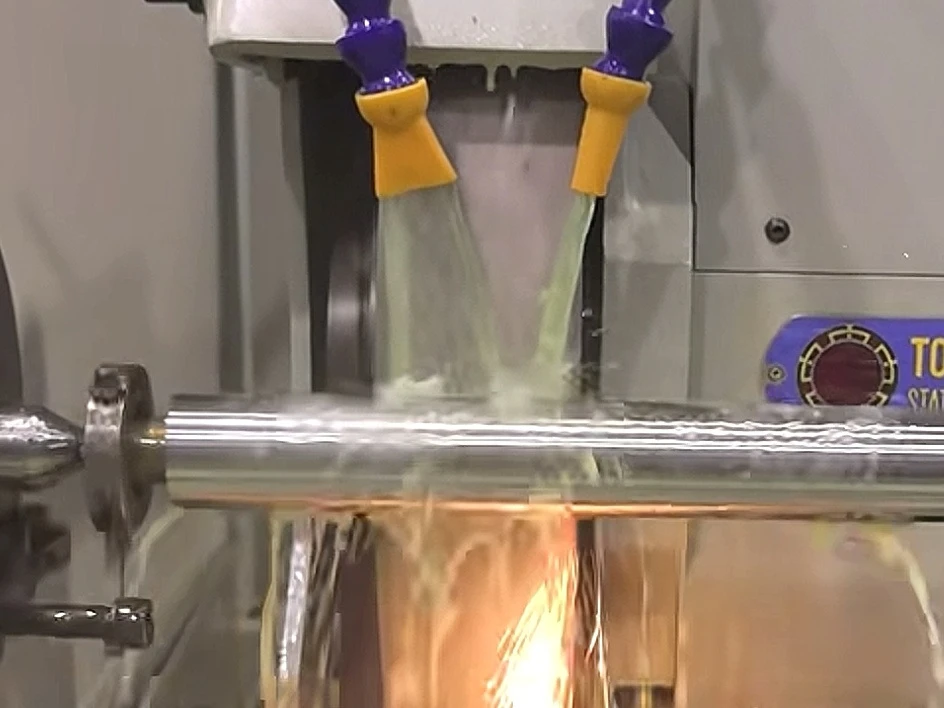
Cylindrical GrindingFine diameter and finish requirements

Grinding refines critical journals, outside diameters and surface finish when a bearing or sealing requirement exceeds the practical turning limit.

Typical Applications: Bearing fits, journals and precision locating diameters

A cylindrical metal shaft being ground with coolant at the grinding wheel

How We Check The Quality Of Your Components

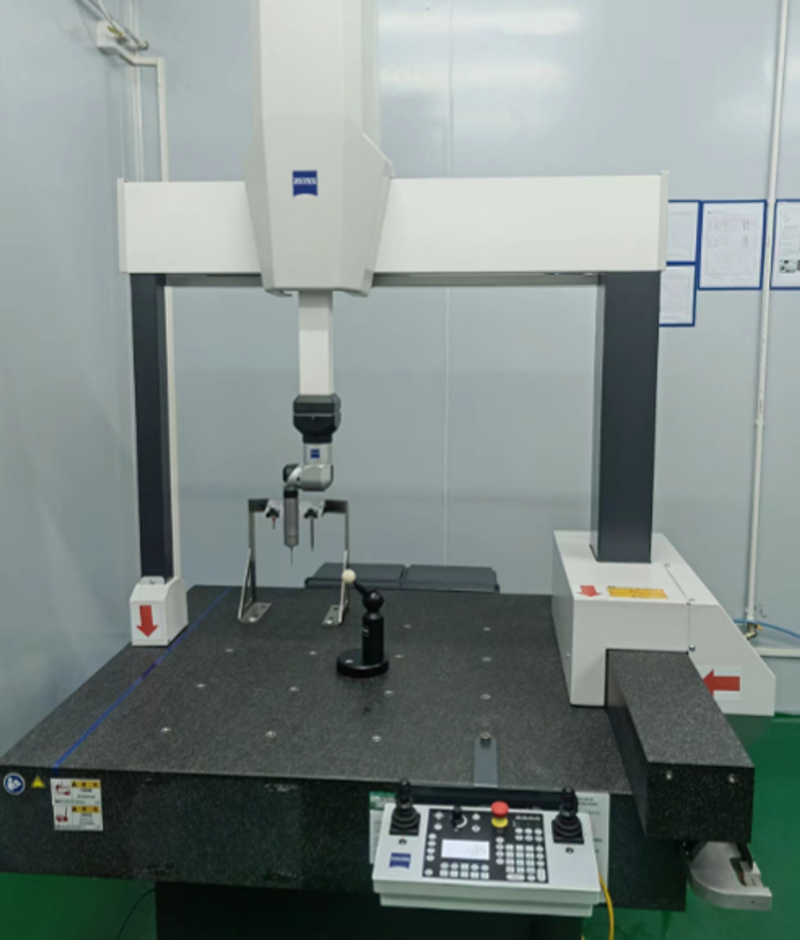
Single-setup machining reduces fixture-to-fixture error, but it does not replace verification. The first part is checked against the released drawing, critical turned and milled features are sampled at defined stages, and final inspection uses calibrated equipment selected for diameter, runout, true position, perpendicularity, profile and surface finish. Zeiss CMM programs support complex relationships, while AS9102 FAI, material certificates, SPC evidence and certificates of conformance are planned when requested at the RFQ stage. Additional checks use 10 microscopes for burrs, edges and surface condition, plus roughness instruments for drawing-defined surface finish.

ZEISS bridge-type coordinate measuring machine with granite table and control console in the factory measurement room

ZEISS CMM

Range
700 × 700 × 600 mm
Quantity
1
Use
3D dimensions, hole positions and geometric relationships.
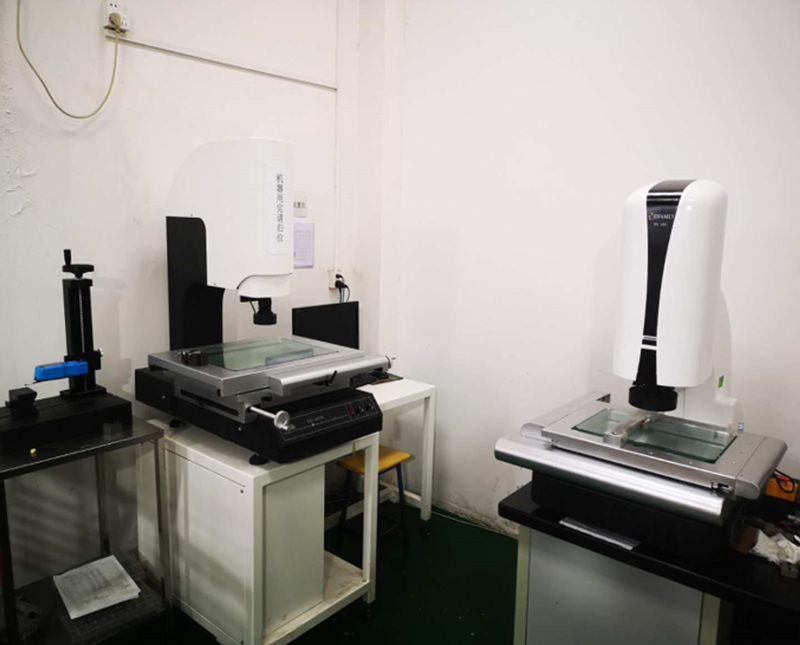
Two optical video measuring machines with glass stages in the factory measurement room

Vision Measuring Systems

Range
200 × 300 mm; 300 × 400 mm
Quantity
2
Use
Non-contact checks of profiles, edges and small features.
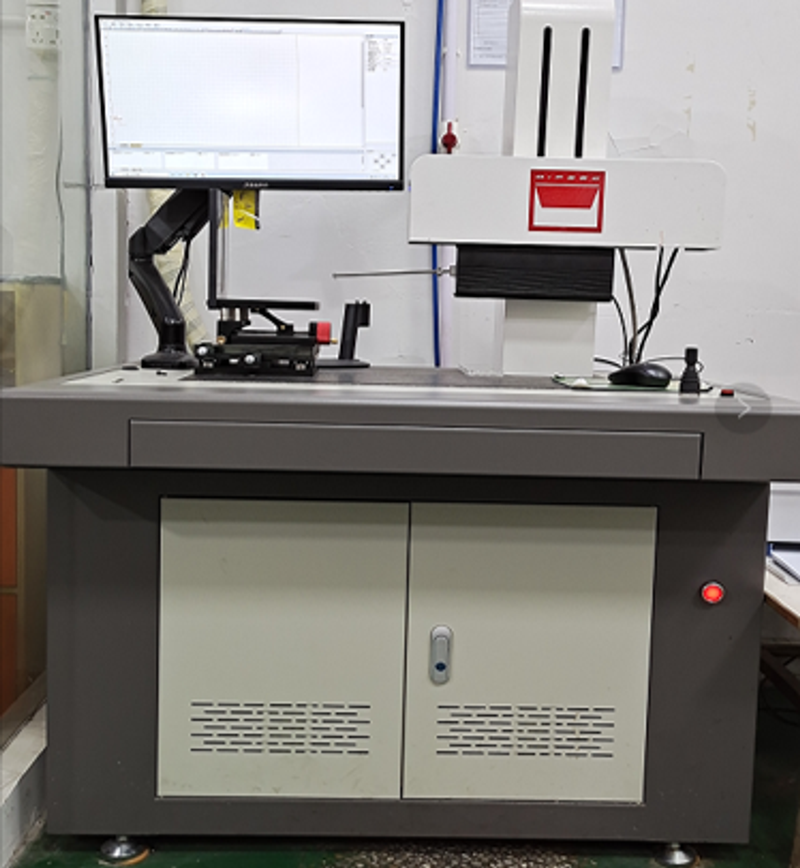
Factory contour measuring instrument with measuring arm, vertical column and computer monitor

Contour Measuring Instrument

Quantity
1
Use
Functional contours and profile geometry.
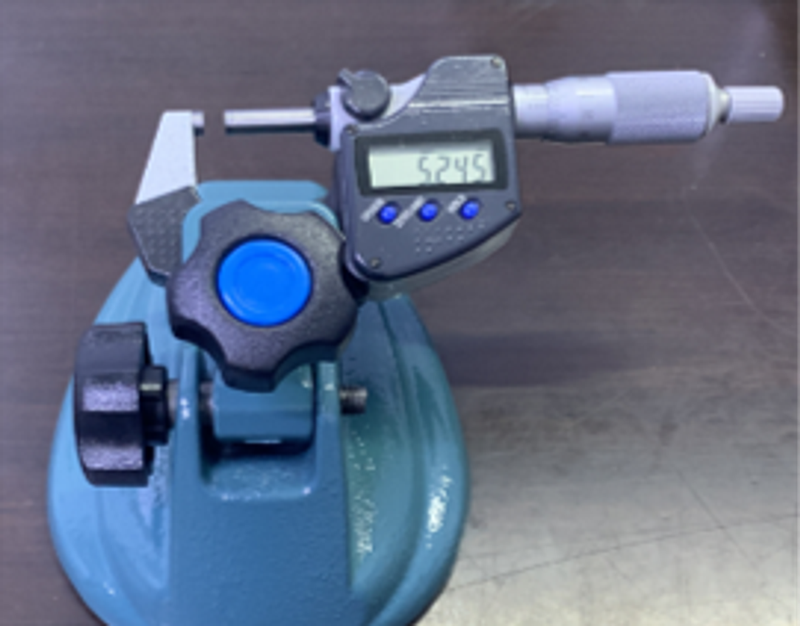
Digital outside micrometer held in a blue bench stand

Micrometers

Range
Outside: selected ranges 0–150 mm; inside: 12–88 mm and 50–600 mm
Use
Outside, inside and feature-specific dimensional checks.
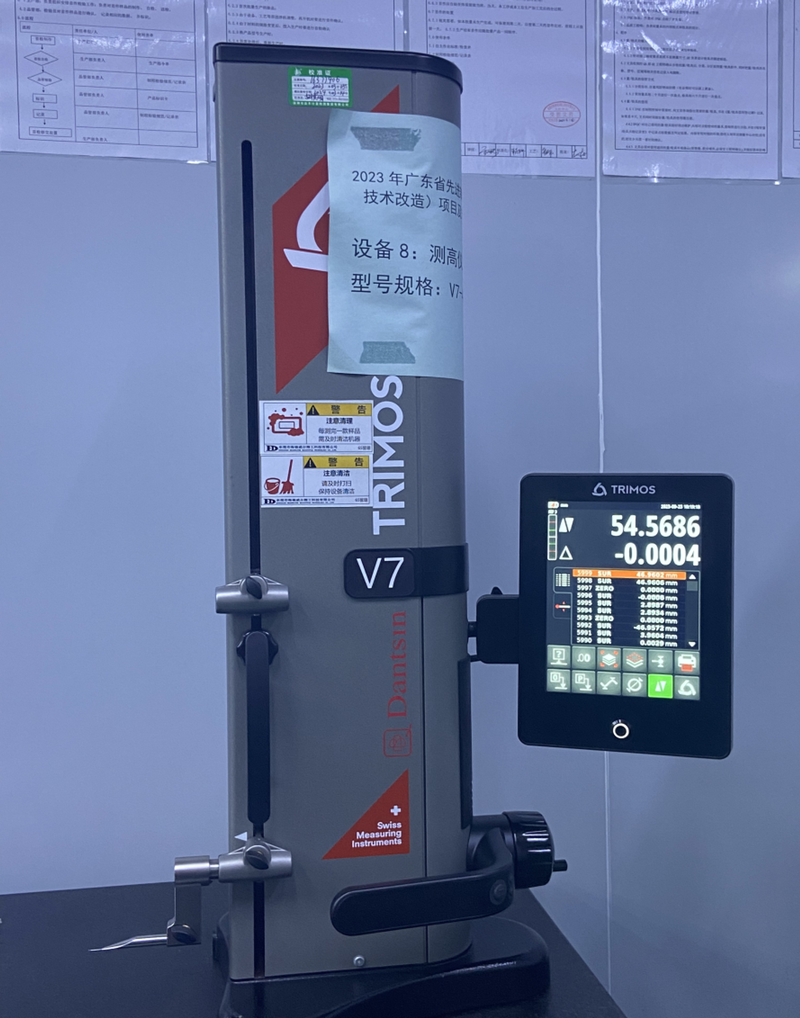
TRIMOS V7 digital height gauge with measuring probe and touchscreen display

TRIMOS V7 Height Gauge

Range
0–400 mm
Quantity
1
Use
Height and comparative dimensions from a reference surface.

Why Choose Our Mill Turning Services?

Our mill-turn service connects process selection, workholding, multitasking equipment, qualified finishing and a measurement room led by a Zeiss CMM. One engineering team follows the drawing from quotation and first-part approval through repeat delivery and documented changes.

  • Single-Setup Feature Relationships

    Turning, milling, drilling and tapping remain on one coordinated route so concentricity, runout and true position depend less on fixture-to-fixture transfer.

  • Dual-Spindle And Multi-Axis Routes

    Back-working on the TSUGAMI and angled-feature access on the DESHAN keep more of the complete component inside the mill-turn cell.

  • Industry-Aligned Validation

    AS9102 FAI, material traceability, drawing-defined inspection and requested production evidence are planned around aerospace, semiconductor, robotics and medical requirements.

  • DFM And Process Selection

    We review whether mill-turn is justified, identify tolerances and features that drive cost, and explain when a simpler turning or milling route is more practical.

  • Inspection Planned Before Cutting

    Turned and milled characteristics receive defined measurement methods, sampling and release evidence before the production program is approved.

  • One Managed Production Route

    Machining, qualified finishing, post-process verification and documentation are coordinated under one purchase order and one responsible engineering team.

Industries We Serve

Mill-turn machining supports industries where mixed rotational and prismatic geometry must be delivered with stable datum relationships, traceable materials and inspection evidence aligned with the drawing and program requirements.

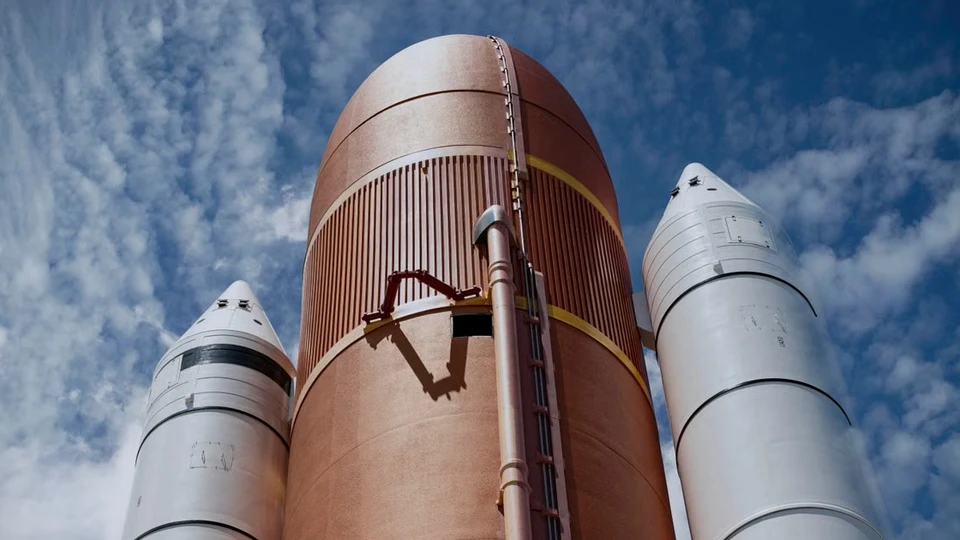
Space launch vehicle tank and boosters against a blue sky

Aerospace

AS9102 first-article planning, material traceability and controlled inspection support tight relationships between turned datums, ports, mounting faces and functional bores.

Ti-6Al-4V · Inconel 718 · 7075-T6

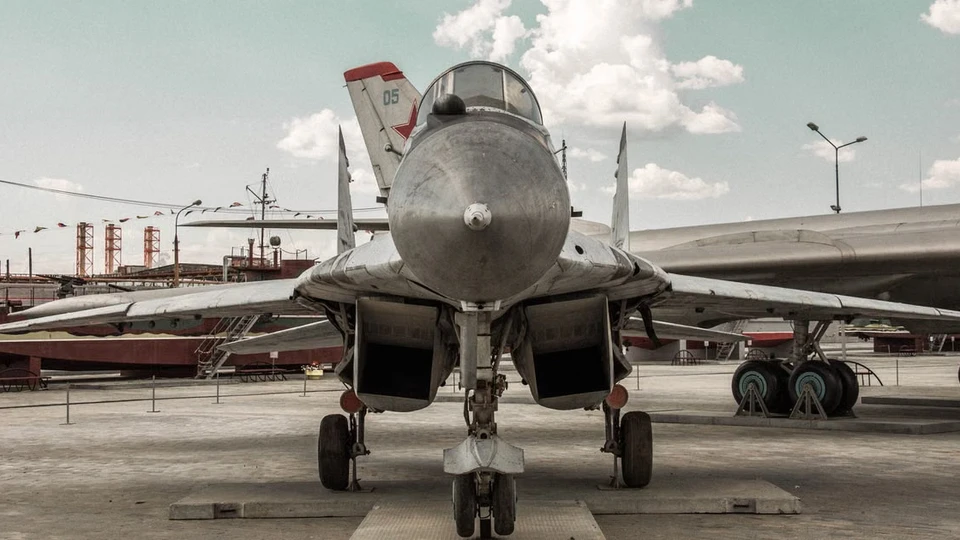
Front view of a military aircraft on outdoor display

Defense

Released revisions, material identity, critical dimensions and retained inspection evidence are controlled around the drawing, purchase order and program requirements.

17-4PH · 7075-T6 · Ti-6Al-4V

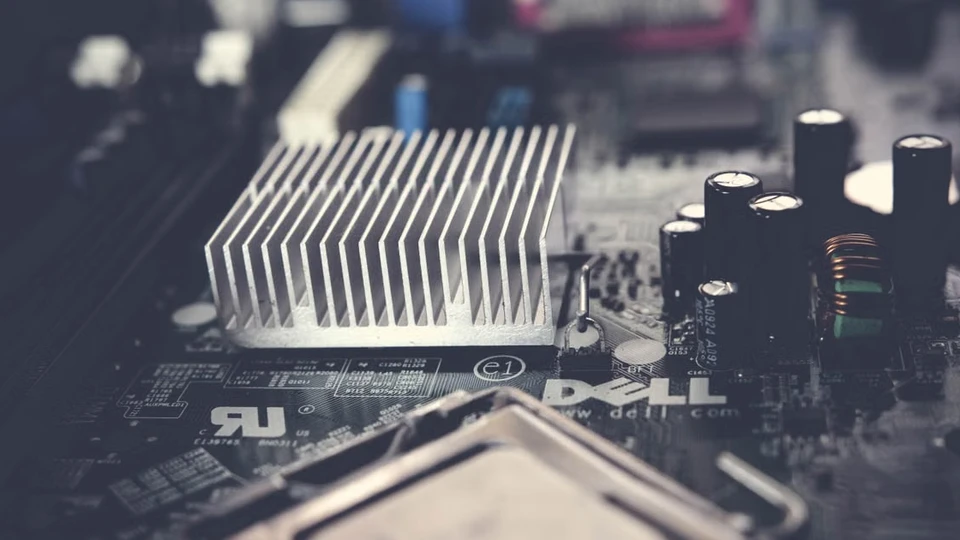
Electronic circuit board with a heat sink and semiconductor components

Semiconductor

Sealing faces, internal passages, surface finish, burr control and material records are planned together for equipment that depends on cleanliness and stable interfaces.

316L · 6061-T6 · copper alloys

Vacuum process chamber with viewing window, pipework and control equipment

Vacuum Systems

Sealing geometry, surface finish, intersecting passages and any specified leak or cleaning requirement are reviewed as part of one manufacturing and inspection plan.

316L · aluminum · engineering plastics

Autonomous wheeled delivery robots beside a building

Robotics

Runout, bearing fits, positional relationships and assembly datums are controlled together where smooth motion and repeatable reducer performance depend on them.

Aluminum · stainless steel · alloy steel

Medical radiotherapy equipment with treatment gantry and patient table

Medical

Customer-defined medical quality controls support traceable materials, burr and edge requirements, controlled finishes and drawing-defined inspection documentation.

316L · Ti-6Al-4V ELI · PEEK

What Is Mill-Turn Machining?

Mill-turn machining, also called turn-mill or multitasking machining, combines a turning spindle with live milling capability and coordinated multi-axis tool movement. The workpiece rotates for diameters, bores, faces and threads, then holds indexed or controlled positions while tools cut flats, pockets, keyways, cross-holes, ports and contours.

The process is designed for components that are fundamentally rotational but carry substantial non-rotational geometry. Instead of moving the part from a lathe to a machining center, turning, milling, drilling, boring, tapping and rear-side work are organized into one setup or as few setups as practical.

Each re-clamping step adds handling time and introduces a new relationship between fixture location and the original datum. Keeping features in one coordinated route helps protect concentricity, runout, true position and perpendicularity where milled details must relate closely to turned surfaces.

Swiss machining is usually preferred for small, slender bar-fed components supported close to the cut. Mill-turn is the stronger choice for larger or chucked parts with more substantial milled geometry. The RFQ review selects the process that best matches the drawing rather than forcing every mixed-geometry part onto the same machine type.

Live milling tool machining a stepped cylindrical component held in a lathe chuck

Frequently Asked Questions

Clear answers about mill-turn process selection, capability, documentation and quoting.

What Is Mill-Turn Machining?

Mill-turn machining combines CNC turning with live milling and multi-axis tool movement. The workpiece rotates for diameters, bores and threads, then holds controlled positions while tools cut flats, pockets, cross-holes, ports and contours.

When Should A Part Use Mill-Turn Instead Of Separate Machines?

Mill-turn is valuable when substantial turned and milled geometry must relate closely to the same datums. Reducing transfers between a lathe and mill removes setup time and lowers the positional risk introduced by re-fixturing.

How Does Mill-Turn Differ From Swiss Machining?

Both can complete complex components in one coordinated machine. Swiss machining is strongest for small, slender bar-fed parts supported close to the cut, while mill-turn handles larger or chucked components with more substantial milled geometry.

What Capacity And Tolerances Can You Support?

The confirmed machine envelope and general tolerance values are listed in the capacity table. Final capability depends on material, wall thickness, feature relationships, tool access, workholding and the agreed inspection method.

Can You Machine From Bar, Forgings Or Castings?

The starting stock is reviewed with the drawing and process route. Bar, prepared blanks, forgings or castings may be suitable depending on geometry, material condition, machining allowance and traceability requirements.

What Quality Documentation Is Available?

Drawing-defined inspection reports, AS9102 first-article records, material certificates, lot traceability, SPC evidence and certificates of conformance can be planned when requested at the RFQ stage.